Pharmaceutical companies increasingly need more from ingredient distributors than product availability and reliable delivery. By connecting customers with formulation expertise, application laboratories, supplier knowledge, and capabilities from adjacent industries, technically equipped distributors can support better-informed ingredient decisions, investigate development problems, and provide additional research and development capacity when internal teams are stretched.
When an Ingredient Request Becomes a Development Question
Pharmaceutical and nutraceutical companies are developing products that use a wider range of ingredients, dosage forms, and delivery formats while responding to changing consumer expectations. At the same time, research and development teams often face compressed timelines and must manage more responsibilities with limited internal resources. These conditions are changing what customers need from their ingredient distributors.
A customer may approach a distributor with what appears to be a straightforward request: Do you have microcrystalline cellulose? A transactional answer would address the available grades, quantities, prices, and delivery timelines. A more useful conversation may begin with the distributor asking another question: What are you making?
Whether the customer is developing a tablet, capsule, powder, topical product, or another dosage form can affect which ingredient is most appropriate. The distributor may also need to understand what function the material must perform, whether the formulation contains moisture-sensitive components, and which processing conditions it will encounter. These questions can reveal that the requested material is appropriate, that another grade may perform better, or that the formulation challenge involves more than ingredient selection.
This approach does not require the distributor to take control of the customer’s formulation or ask for unnecessary proprietary information. The customer determines how much information to share and retains responsibility for development decisions. When greater disclosure is useful, the parties can work under a nondisclosure agreement. The distributor’s role is to help clarify the request, identify relevant options, and connect the customer with additional technical resources when needed.
A Technical Bridge Into a Broader Network
At Ingredients + Specialties from Univar Solutions, an application development specialist (ADS) serves as a technical bridge among the customer, the account manager, ingredient manufacturers, product specialists, our Solution Centers, and other technical resources across our organization.
The account manager remains an important commercial contact for questions about pricing, samples, inventory, and availability. The ADS adds a technical perspective by examining how the requested ingredient relates to the formulation, process, dosage form, and intended product attributes. If the question requires more specialized knowledge, the ADS can bring in a supplier representative, product manager, laboratory scientist, or subject matter expert from another application area.
This coordination can simplify interactions that might otherwise require a customer to contact several ingredient manufacturers and technical teams independently. The ADS helps direct each question to the appropriate resource, maintains continuity across those conversations, and translates the resulting information into a response relevant to the customer’s application.
The same relationship can simplify access to specifications, quality documentation, supplier information, and other materials needed to evaluate an ingredient. Ingredients + Specialties from Univar Solutions does not assume the customer’s regulatory responsibilities, but we can coordinate information across suppliers and help customers obtain documentation for their own quality and regulatory assessments.
This technical bridge becomes particularly valuable when the customer knows what it wants the product to accomplish but has not yet determined which ingredient, grade, or processing approach offers the best path forward. Rather than presenting an undifferentiated catalog of options, the distributor can help narrow the field according to the customer’s stated requirements.
Preserving Options Before the Formulation Is Locked
Apparently similar excipients can perform differently once incorporated into a formulation or manufacturing process. Differences in particle size, moisture content, density, flow, compactability, or compatibility with other materials may affect whether an ingredient succeeds in a specific application.
Direct compression provides a useful example. A formulation team may be evaluating multiple grades of microcrystalline cellulose, mannitol, or co-processed excipients from different manufacturers. Selecting among them requires more than confirming that each material belongs to the correct excipient category. The team may need to consider how the grade interacts with the active pharmaceutical ingredient (API), whether it provides adequate flow and compression performance, and how its moisture profile affects the overall formulation.
Particle size can be particularly important. When a micronized API is combined with much larger excipient particles, the materials may separate during handling or processing. The mixture can begin to behave like sand and rocks in the same container, with the smaller particles settling into spaces between the larger ones. That segregation can undermine content uniformity even when each ingredient is individually suitable for pharmaceutical use.
Environmental conditions add another layer of complexity. A formulation that performs well under controlled laboratory conditions may behave differently when manufactured, stored, transported, or used in a hot and humid environment. If the API or finished formulation is moisture-sensitive, a low-moisture excipient or another grade may offer advantages that would not be apparent from the basic ingredient description.
Technical discussion early in development can help the customer compare these variables before the formulation and process become difficult to change. Samples can support screening work, while laboratory comparisons and prototypes can provide evidence about how candidate materials behave under relevant conditions. This support does not eliminate the customer’s own development work, but it can help preserve options and direct internal resources toward the most promising candidates.
Additional R&D Capacity Across Technical Boundaries
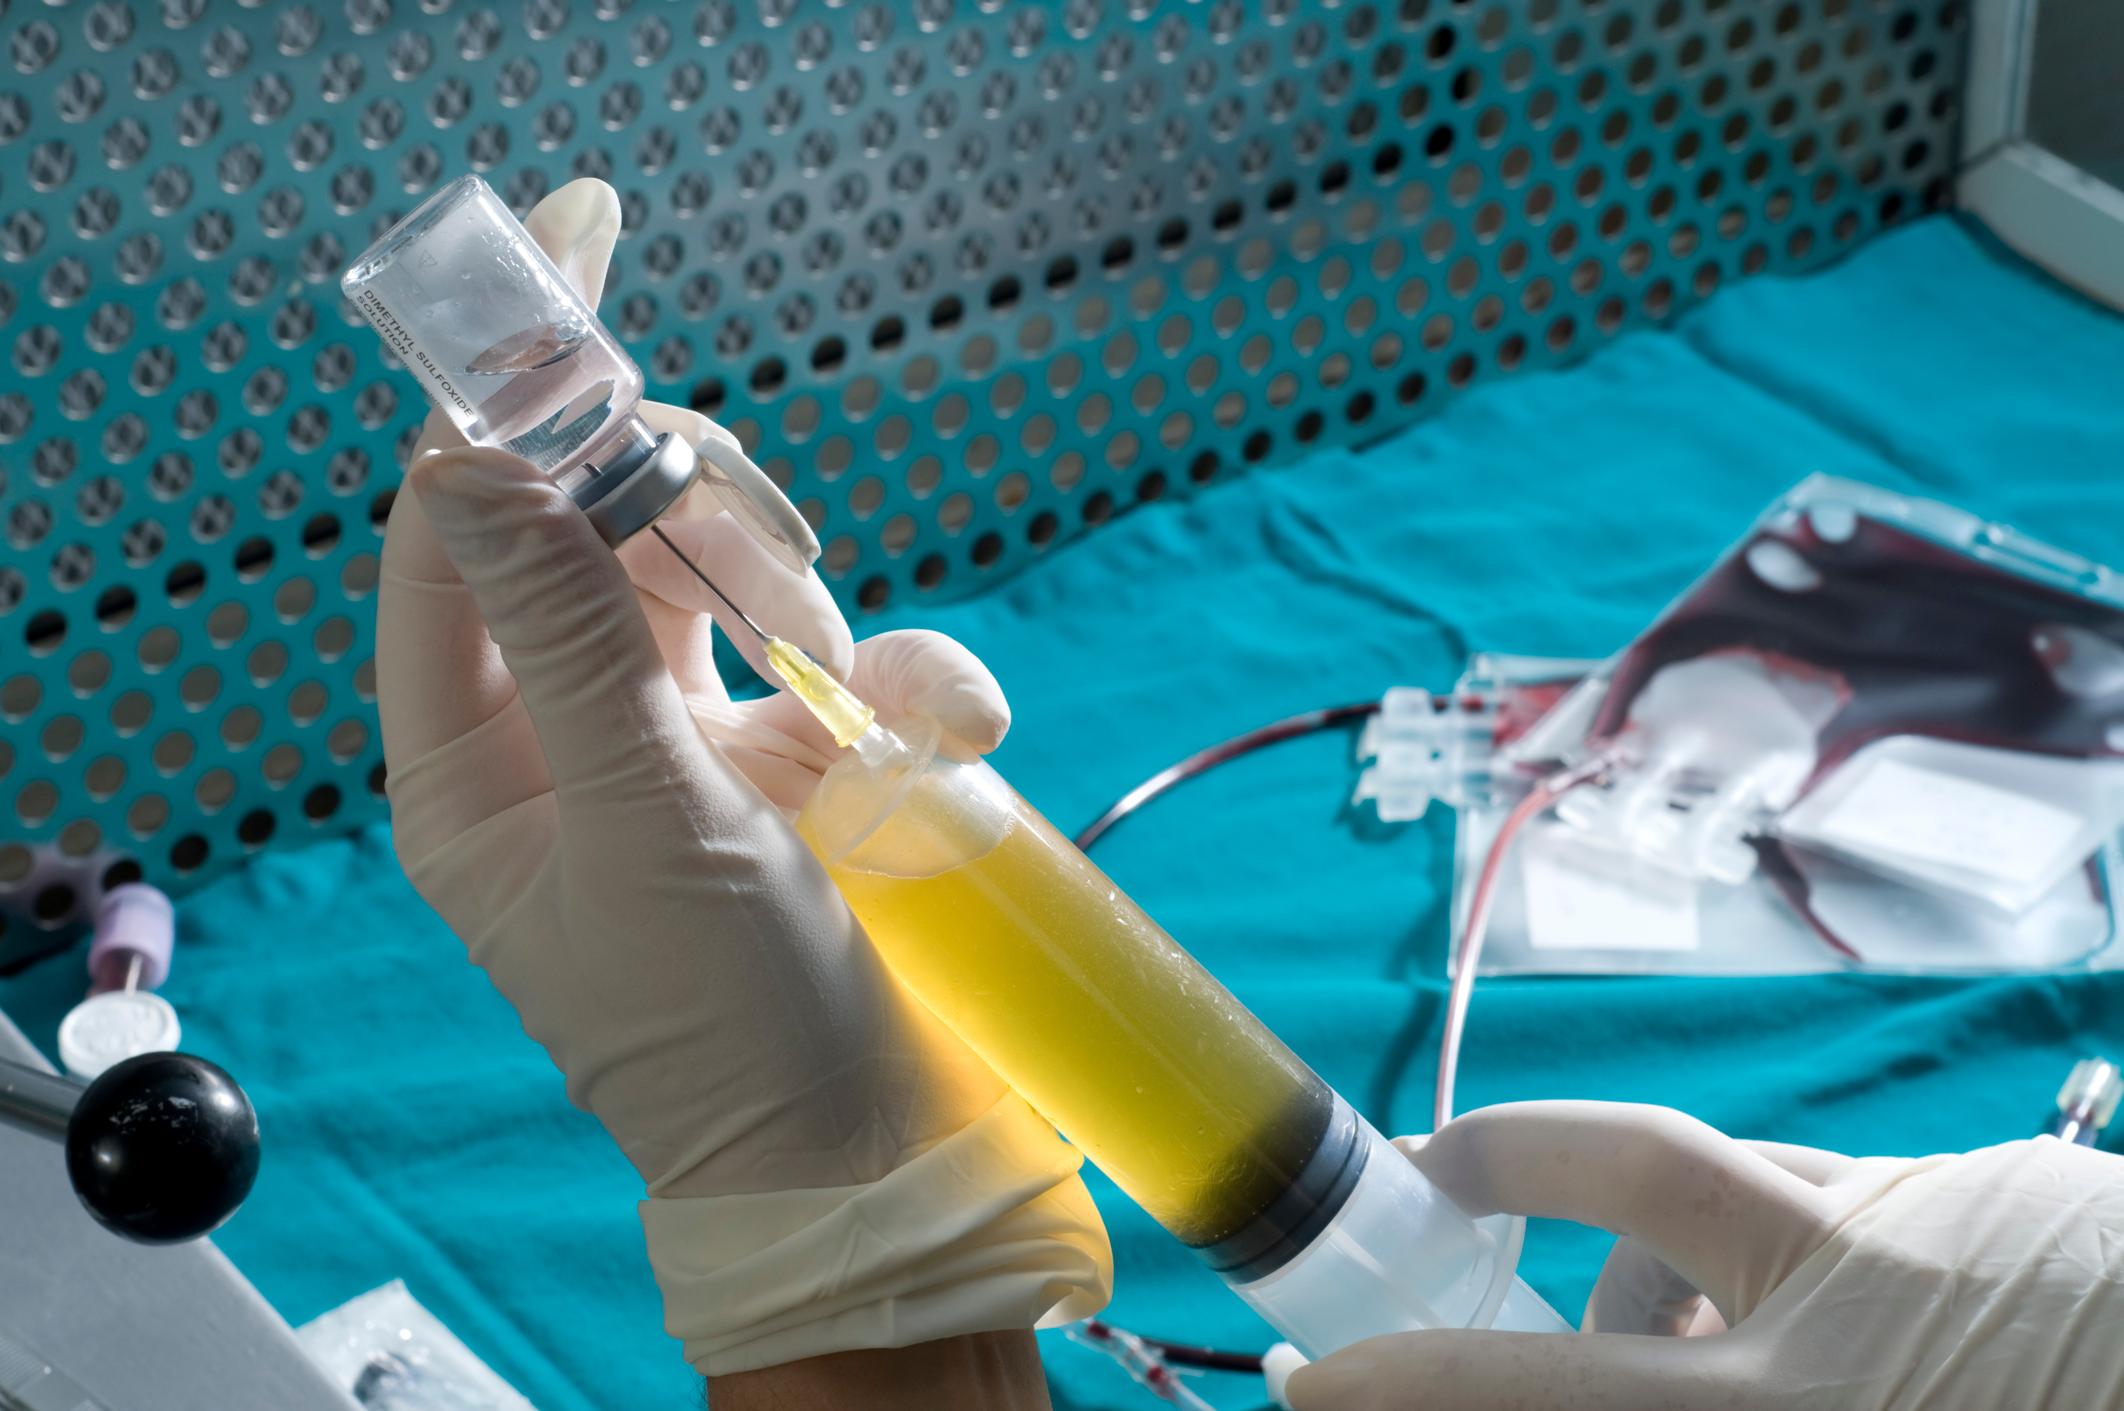
When a question requires experimental work, our Solution Centers can provide defined laboratory support without assuming ownership of the customer’s development program. The work begins with the customer’s question and may include comparative ingredient assessments, prototype development, troubleshooting, or evaluation of process variables.
The resulting work can be documented in a detailed report describing the materials, methods, observations, and findings. This gives the customer more than an informal recommendation. It provides information that its development team can evaluate, reproduce, and use to determine the next step.
For a company with a lean R&D group, this laboratory access can provide additional capacity at a point when internal scientists are balancing several projects and deadlines. A larger organization may use the same resources to investigate a specific issue without diverting equipment or personnel from higher-priority programs. In both situations, the customer remains responsible for deciding how the findings will influence development.
The available expertise also extends beyond conventional pharmaceutical formulation. A nutraceutical customer developing a gummy, for example, may benefit from food-science capabilities at The Hatchery in Chicago. A company working on a topical pharmaceutical product may need to understand sensory properties, spreadability, or other attributes routinely evaluated in beauty and personal-care applications. A hydrocolloid medical device may require knowledge of both pharmaceutical materials and adhesive technologies.
The hydrocolloid example demonstrates how a distributor can coordinate technical groups that do not ordinarily sit within the same customer project team. Equipment, application knowledge, and formulation experience developed for one industry may help answer a problem arising in another, provided that the work remains aligned with the customer’s technical, quality, and regulatory requirements.
The ADS makes this model workable by framing the customer’s question and identifying the right combination of resources. The customer does not need to determine in advance which laboratory, discipline, or specialist should investigate the issue.
When the Initial Request Is Not the Final Solution
Some of the most useful technical engagements begin when the requested approach does not work as expected. In one nutraceutical project, a customer needed to combine an active ingredient with a required oil. Directly mixing the two materials did not produce a viable formulation.
The customer’s initial question focused on how to make those ingredients work together. Laboratory investigation at one of our Solution Centers led to a different solution: placing the active ingredient in a smaller capsule and then enclosing that capsule within a larger capsule containing the oil. This capsule-in-capsule format kept the incompatible components separated while allowing them to remain part of the same finished product.
Access to a broader technical network can reveal a workable route when the originally requested formulation approach proves unsuitable. The most useful answer may involve reconsidering the delivery format rather than continuing to adjust the original mixture.
Troubleshooting can also require examining what happens after a product leaves the development laboratory. In another case, a ready-to-mix powder was manufactured in South Florida and shipped to markets in Central and South America. The formulation performed as expected where it was developed, but customers encountered problems under the hot, humid conditions in which the product was ultimately stored and used, sometimes without air conditioning.
Looking only at the original formula would have provided an incomplete picture. The investigation also needed to consider packaging, transportation, storage, local climate, and how consumers handled the product after opening it. These factors can change the behavior of moisture-sensitive powders even when the formulation itself appears sound under controlled conditions.
Cases like these illustrate why technical troubleshooting must begin with the conditions surrounding the problem. The answer may involve an ingredient change, a different grade, modified processing conditions, another dosage format, or closer attention to packaging and use. Defining the real question is often the first step toward finding a practical response.
Extending Innovation Across Different Customer Types
Ingredient manufacturers continually introduce new excipients, functional ingredients, processing aids, and material grades. The value of those innovations depends partly on whether developers learn about them and understand where they may be useful.
Distributors can help connect supplier innovation with relevant applications. Because they work across multiple manufacturers and customer groups, they can identify where a new ingredient may address a recurring formulation challenge, support a developing consumer preference, or offer another option for a particular dosage form. They can also communicate supplier updates and provide samples, documentation, and technical information needed for an initial evaluation.
This role has become increasingly relevant in nutraceutical and consumer-health markets, where demand can change quickly. Interest in plant-based capsules, organic ingredient blends, ingredient origin, and personalized nutrition can create new formulation requirements. A customer may need to evaluate whether an alternative ingredient can deliver the expected performance while supporting the product positioning consumers want.
The model must also account for differences among customer organizations. Large pharmaceutical companies may have extensive internal formulation, analytical, procurement, and regulatory teams, yet still need external support for a specialized question or a time-sensitive project. Emerging and smaller companies may have fewer internal resources and less direct access to ingredient manufacturers.
Order volume can affect how those smaller customers obtain materials. The minimum order quantity available through Ingredients + Specialties from Univar Solutions may exceed what an early-stage company needs for development or limited production. In those situations, regional distributors can supply smaller quantities. Because we maintain relationships with these distributors, they can also escalate technical questions when their customers encounter formulation or processing problems.
This extended network helps move ingredient information and technical support beyond companies with the largest purchasing volumes. It also gives supplier partners a route to customer groups they may not reach efficiently through direct relationships alone.
Connecting Technical Decisions With Supply Continuity
The expanded technical role does not reduce the importance of dependable sourcing and logistics. Product availability, consistent quality, accurate documentation, and reliable delivery remain the foundation of the distributor relationship. Technical recommendations have limited value if the selected material cannot be supplied in the quantity, location, or timeframe required.
Supply conditions can also affect development decisions earlier than they once did. Geopolitical instability, transportation disruptions, fuel costs, severe weather, and changes in raw material availability can alter lead times and pricing. Compressed development schedules may require procurement and supply teams to evaluate those factors while formulation work is still underway.
Customers can reduce exposure by identifying single-source dependencies, examining geographic concentration, evaluating alternative suppliers, and determining where safety stock may be justified. Dual sourcing can provide additional flexibility, although an alternative ingredient or supplier must still meet the product’s technical, quality, and regulatory requirements. A nominal substitute is not automatically interchangeable within a validated formulation or process.
This is where technical and supply considerations intersect. A distributor familiar with the formulation’s functional requirements can help identify potential alternatives, obtain the relevant samples and documentation, and coordinate communication with suppliers. The customer must conduct the necessary qualification and change-control activities, but earlier visibility can preserve more options if conditions change.
Distributor relationships can also provide information about availability, lead times, pricing, and emerging supply constraints. That visibility helps customers assess risk and make sourcing decisions with a clearer understanding of both immediate requirements and future demand. Ingredient selection, supplier qualification, inventory planning, and geographic diversification can then support both development and continued supply.
A Relationship That Expands When Needed
A modern distributor relationship does not need to become an extensive technical project every time a customer places an order. Sometimes the customer knows exactly which approved ingredient it needs, and the most valuable response is accurate information about availability, price, and delivery.
At other times, the initial request reveals a broader question. The customer may need to compare excipient grades, investigate a formulation problem, understand why a material behaves differently under certain conditions, or access equipment and expertise outside its own laboratory. That broader support gives customers access to additional resources when needed, without requiring them to create every capability internally or begin a separate provider search whenever an unusual problem emerges.
At Ingredients + Specialties from Univar Solutions, that model connects account management, ingredient and supplier knowledge, application development specialists, Solution Centers, and expertise across multiple industries. The result is a distributor relationship grounded in reliable fulfillment that can extend into formulation support, laboratory investigation, and collaborative problem-solving whenever a customer needs more than an ingredient delivered.